
1.2379 cold work tool steel

1.2379 steel, also known as D2 steel, is a high-carbon, high-chromium cold work die steel that can be heat treated to 60-62 HRC. Due to the large amount of carbides in the microstructure, it has excellent wear resistance. Suitable for manufacturing high-strength parts such as cold work dies, cutting tools and stamping dies. Its high chromium content provides good corrosion resistance, allowing it to maintain stable performance in harsh working environments. At the same time, its heat treatment properties are also very good, and the required hardness and toughness can be obtained through appropriate heat treatment. 1.2379 steel has stable mechanical properties, high tensile strength and yield strength, and can withstand larger loads. In addition, 1.2379 steel also has excellent cutting performance and can maintain long tool life under high-speed cutting conditions. Its high hardness and excellent cutting stability make it an ideal material for manufacturing molds and cutting tools.
1.2379 steel is widely used in long production cold working applications requiring very high wear resistance and high compressive strength. It can be machined in the annealed condition and, like other air-hardening tool steels, exhibits minimal distortion during heat treatment. In general, 1.2379 steel has become a cold work die steel widely used in industrial fields due to its excellent chemical composition and performance. Its high carbon and high chromium content gives it excellent hardness, wear resistance and corrosion resistance, allowing it to maintain stable performance in various harsh environments. Whether it is manufacturing molds or cutting tools, 1.2379 steel can exert excellent cutting performance and improve work efficiency.
Similar brands at home and abroad: American D2, Chinese Cr12Mo1V1, German 1.2379, Japanese SKD11, Austrian Bailuk K110.
Heat treatment process:
Stress relief annealing: After rough machining, the workpiece is heated to 600~650℃, kept for 2 hours, cooled to 500℃ in the furnace, and air cooled after exiting the furnace.
Quenching: The workpiece is slowly heated to 600°C, kept for 20 minutes for the first preheating, and then raised to 850°C after equalization, and then kept for 30 minutes for the second preheating, and finally heated to 1020~1040°C, kept for 25~40 minutes, and discharged. Air cooled.
Tempering: Tempering should be carried out immediately after quenching, and tempered at least twice, with a holding time of not less than 2 hours each time.
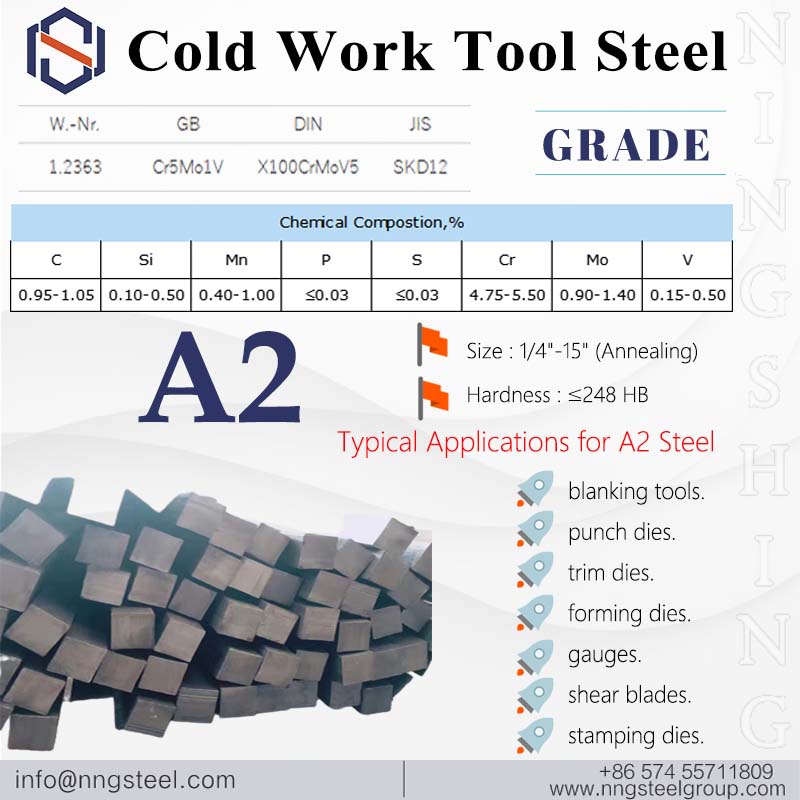 Cold working tool steel-A2
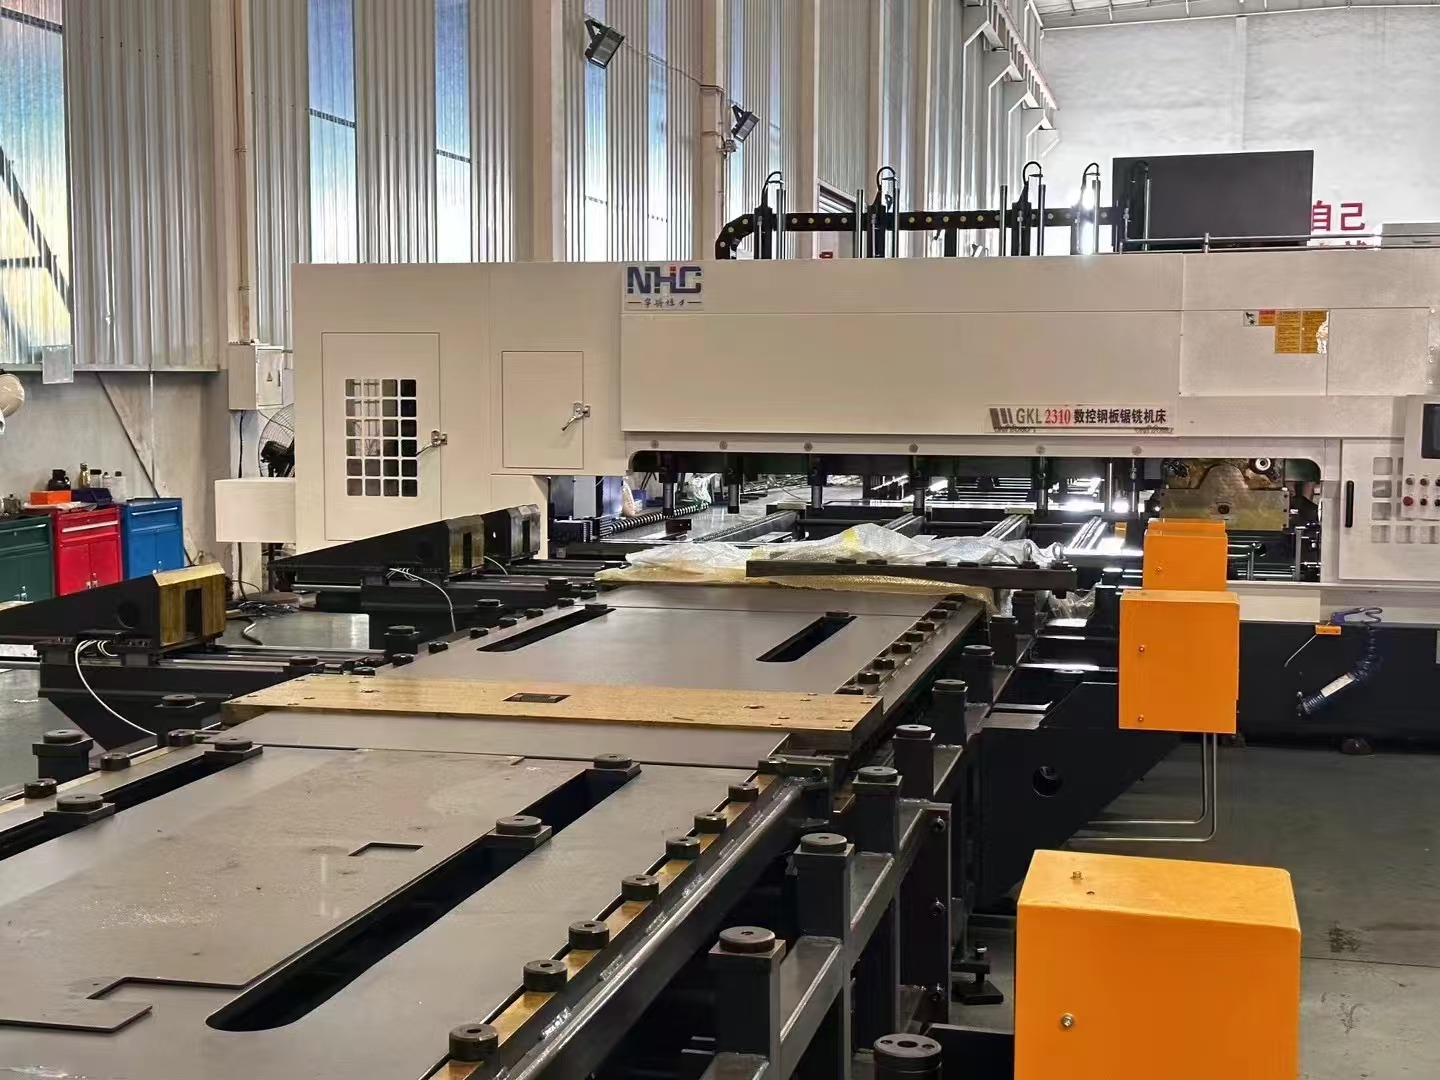 Ningshing circular saws - the sheet metal processing specialists
 Ningshing in Process Gauge
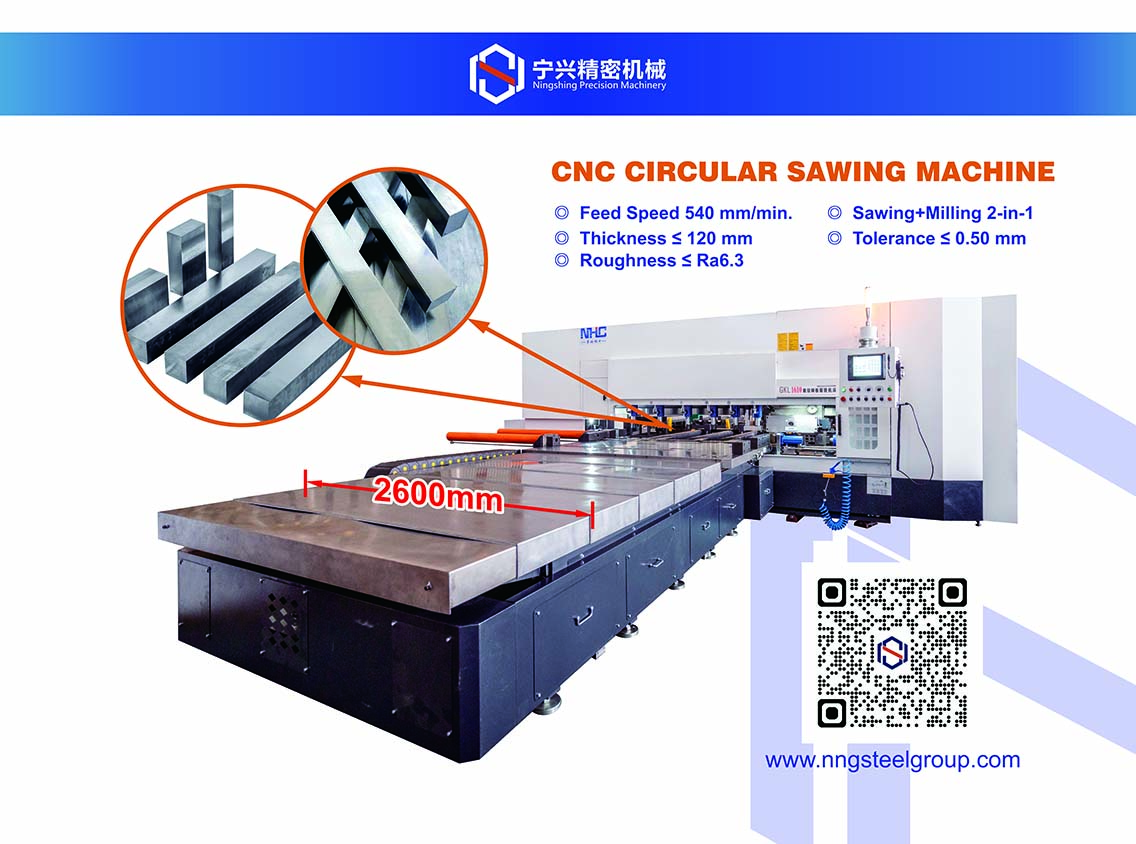 CNC circular sawing machines help increase your productivity
 The leading special steel distributor in China-Ningshing
 Trusted Steel Supplier-Ningshing
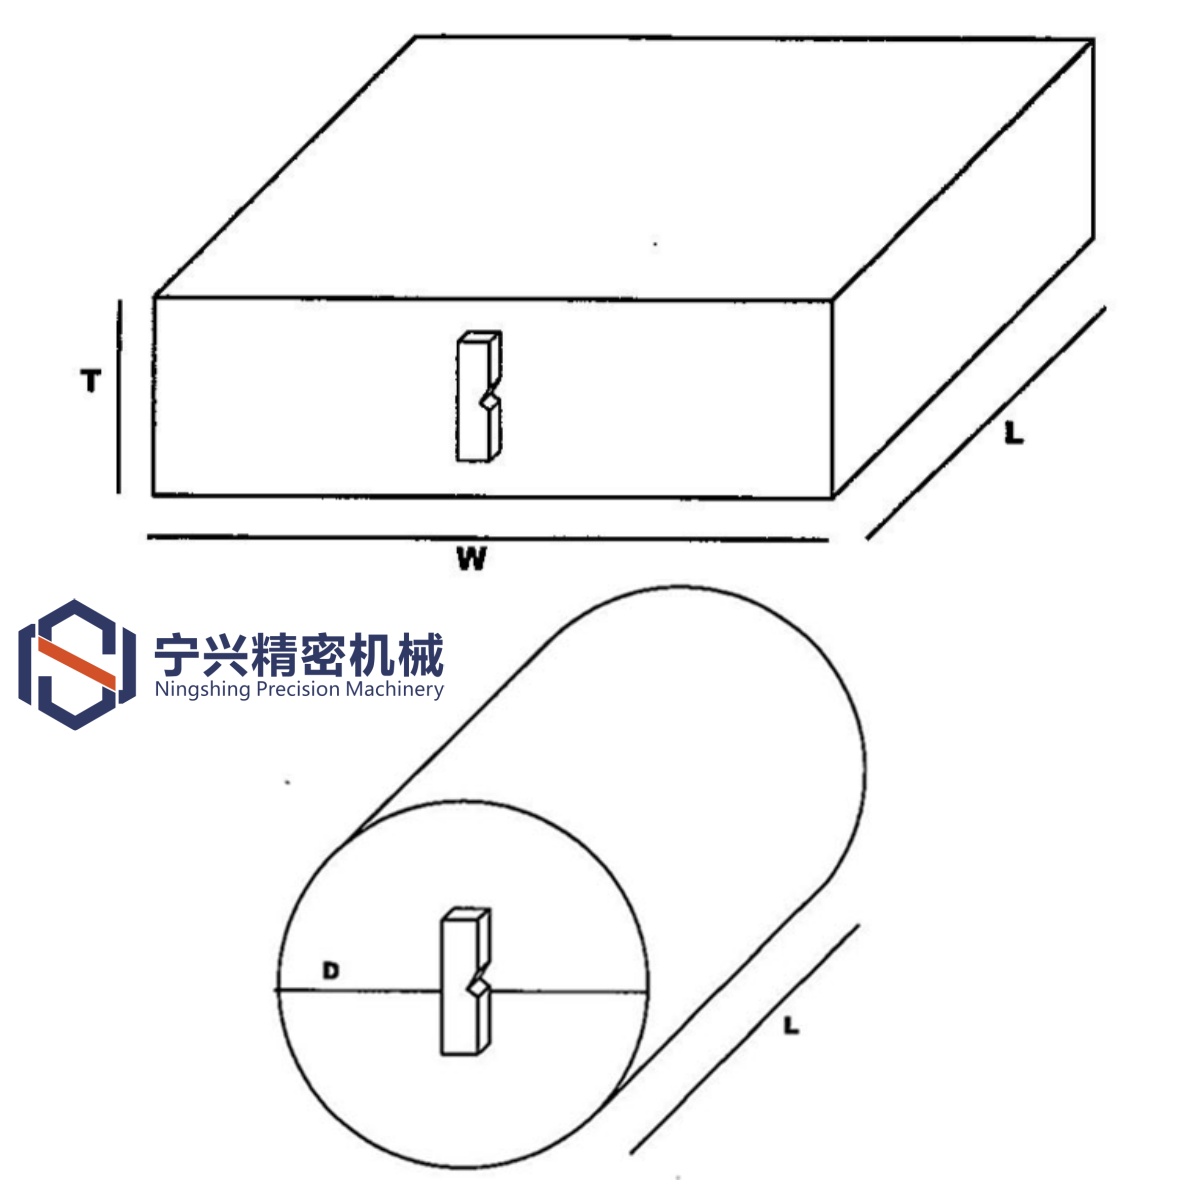 Normative and accurate specimen preparation of Ningshing
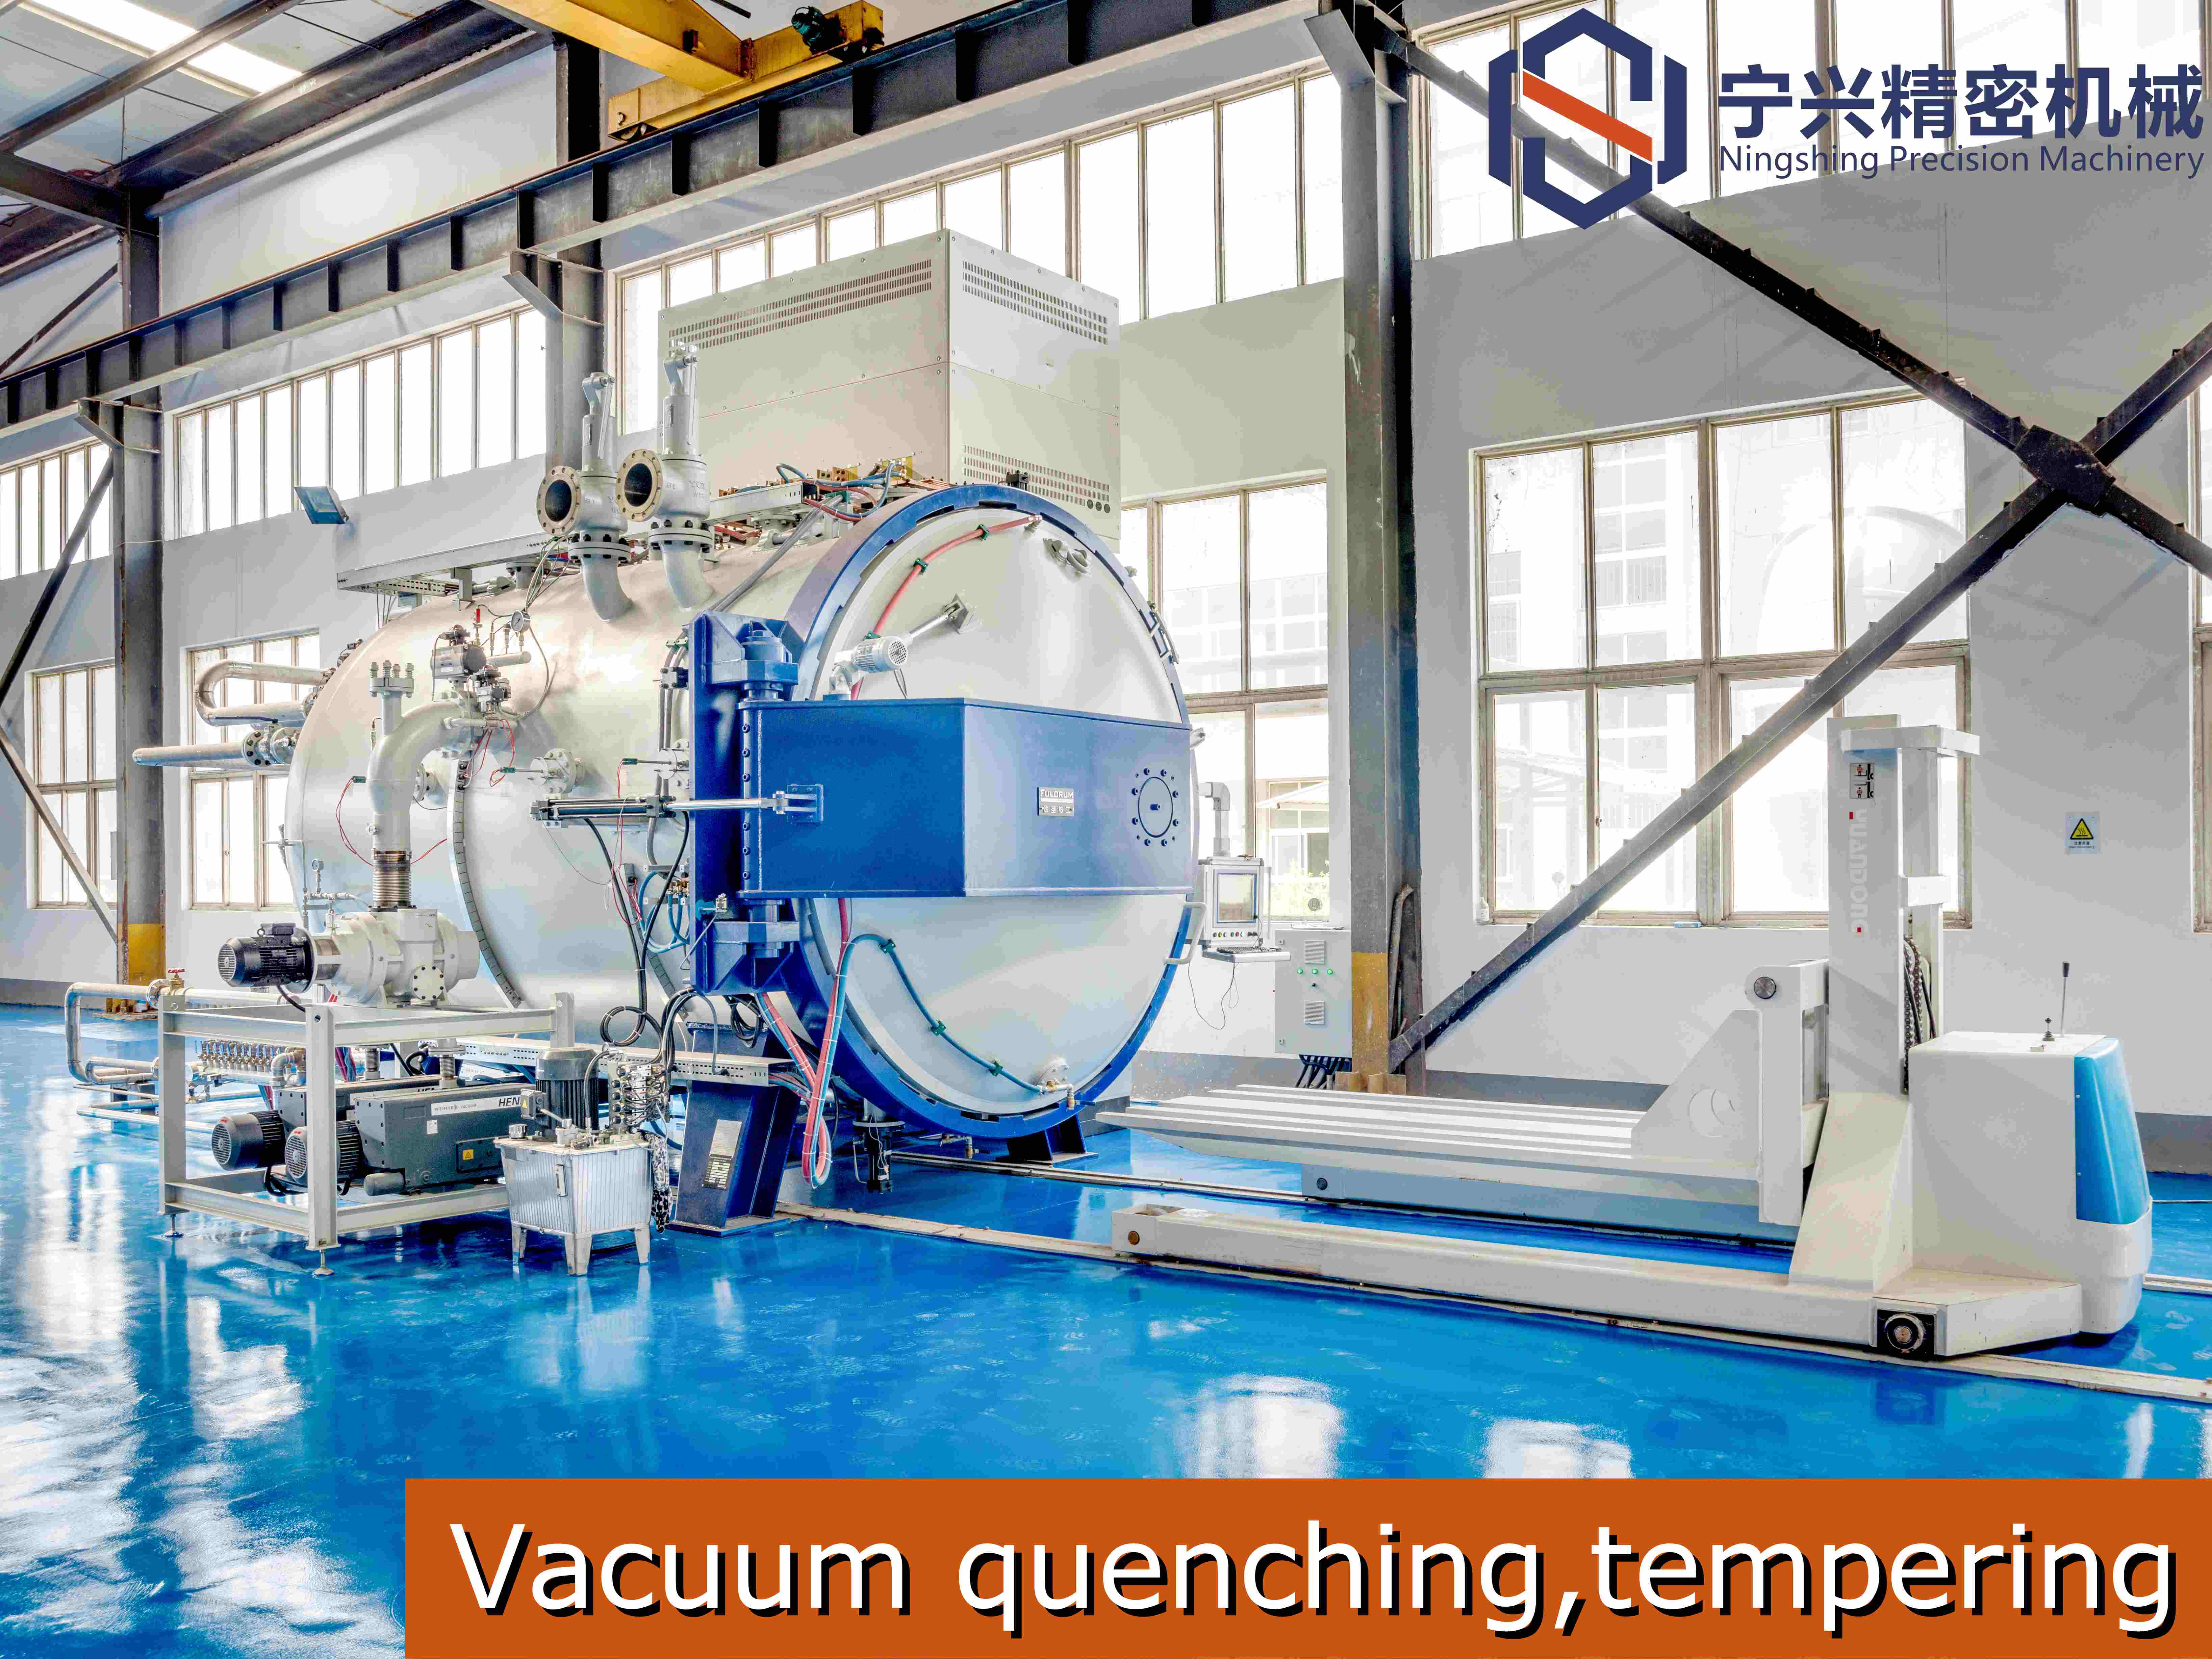 Ningshing Heat Treatment Program: A Key Process for Enhancing Material Properties
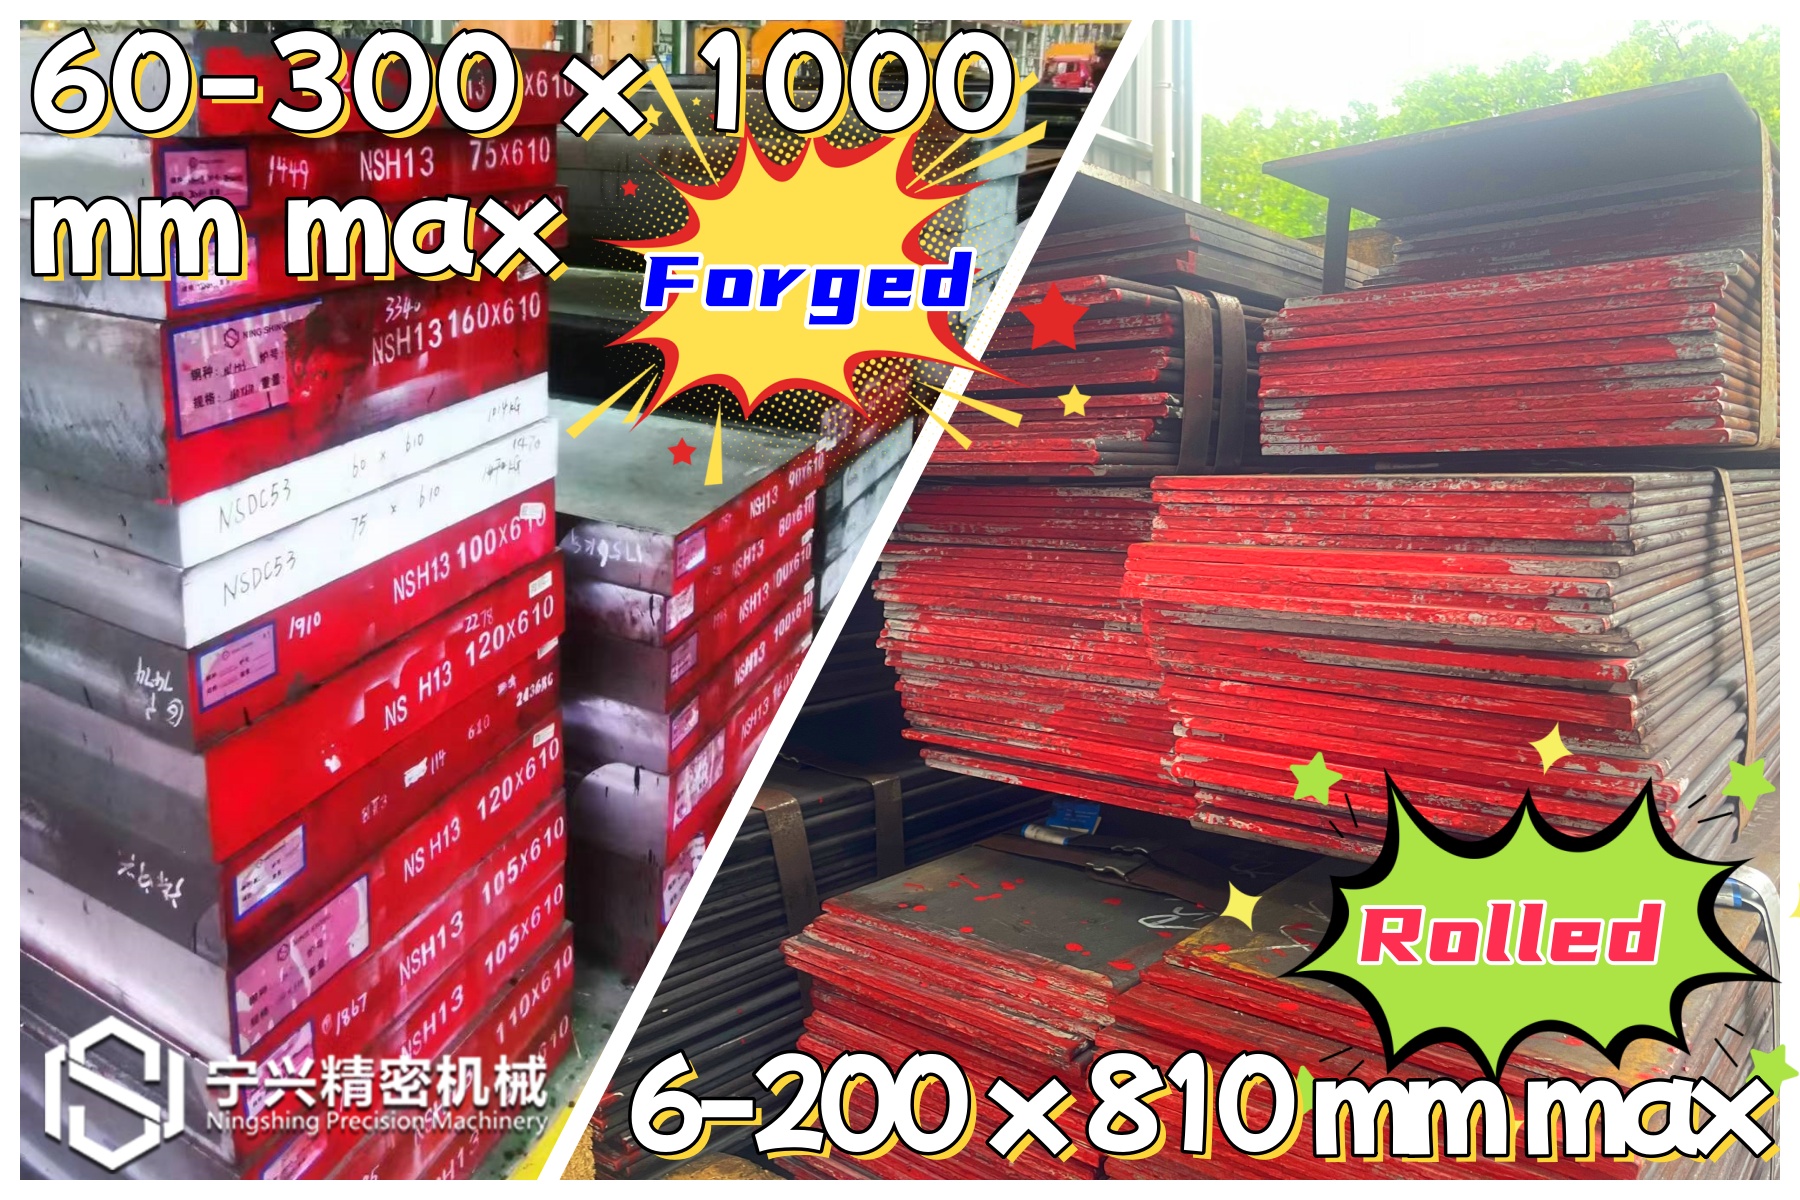 Ningshing hot work steels NS2344
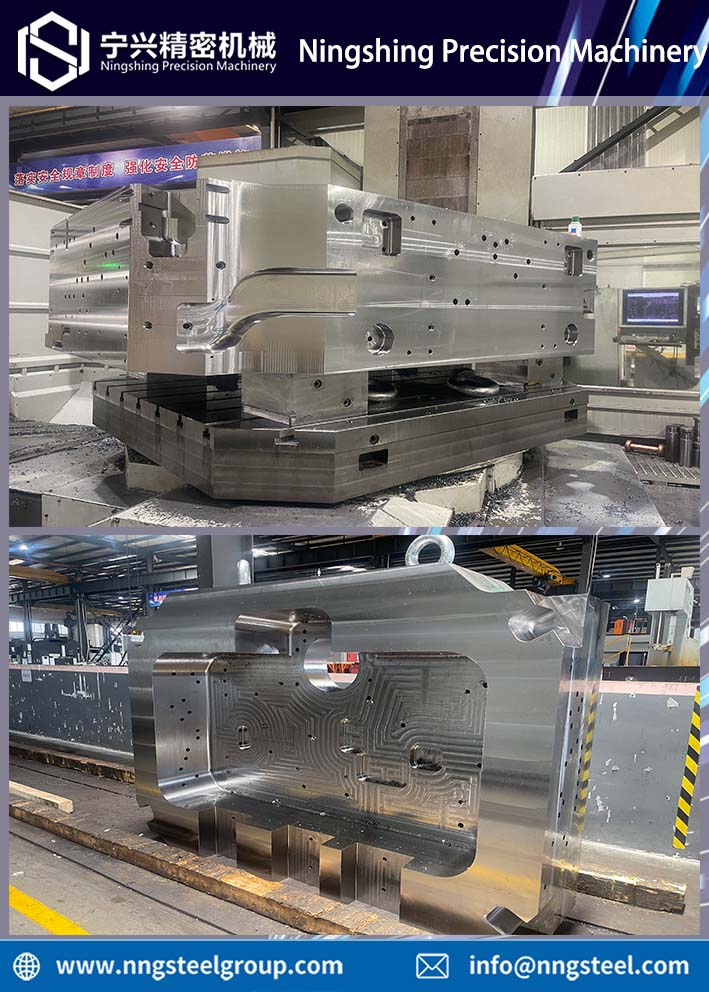 Die casting mold applications
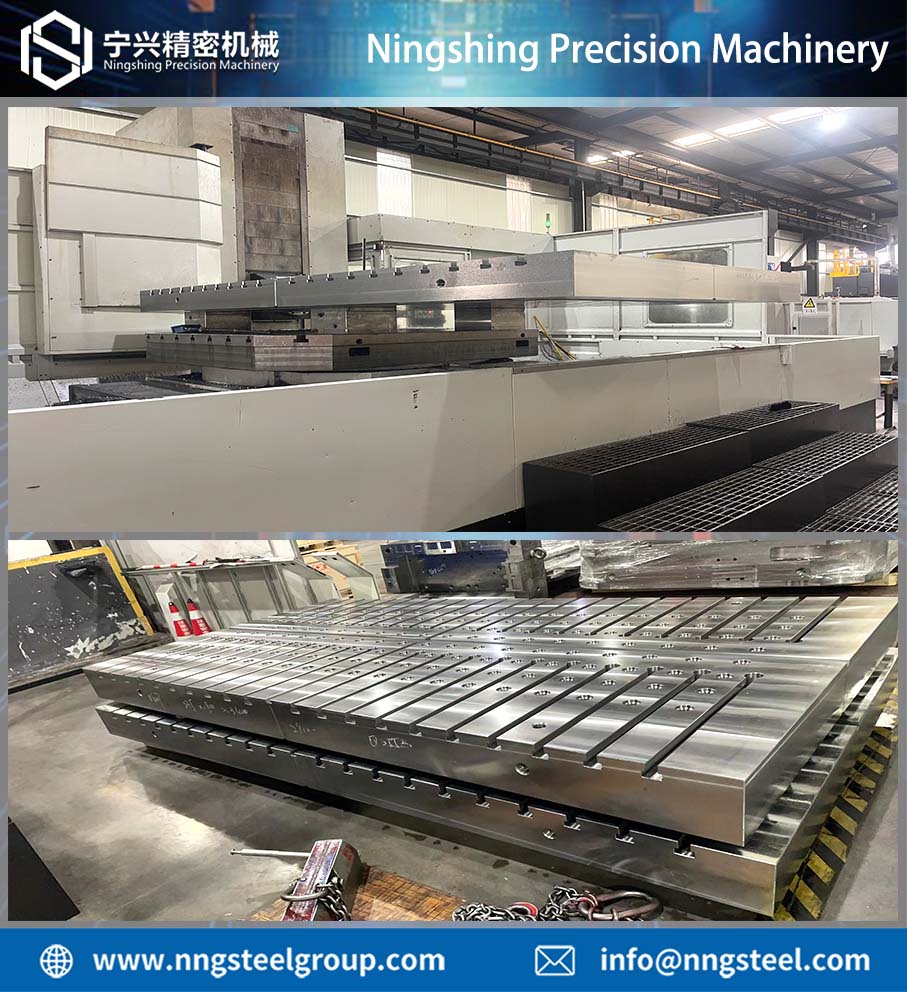 【The Power of Manufacturing】 Providing Unbreakable Support for Press Machine—— Our Bolster Plate!
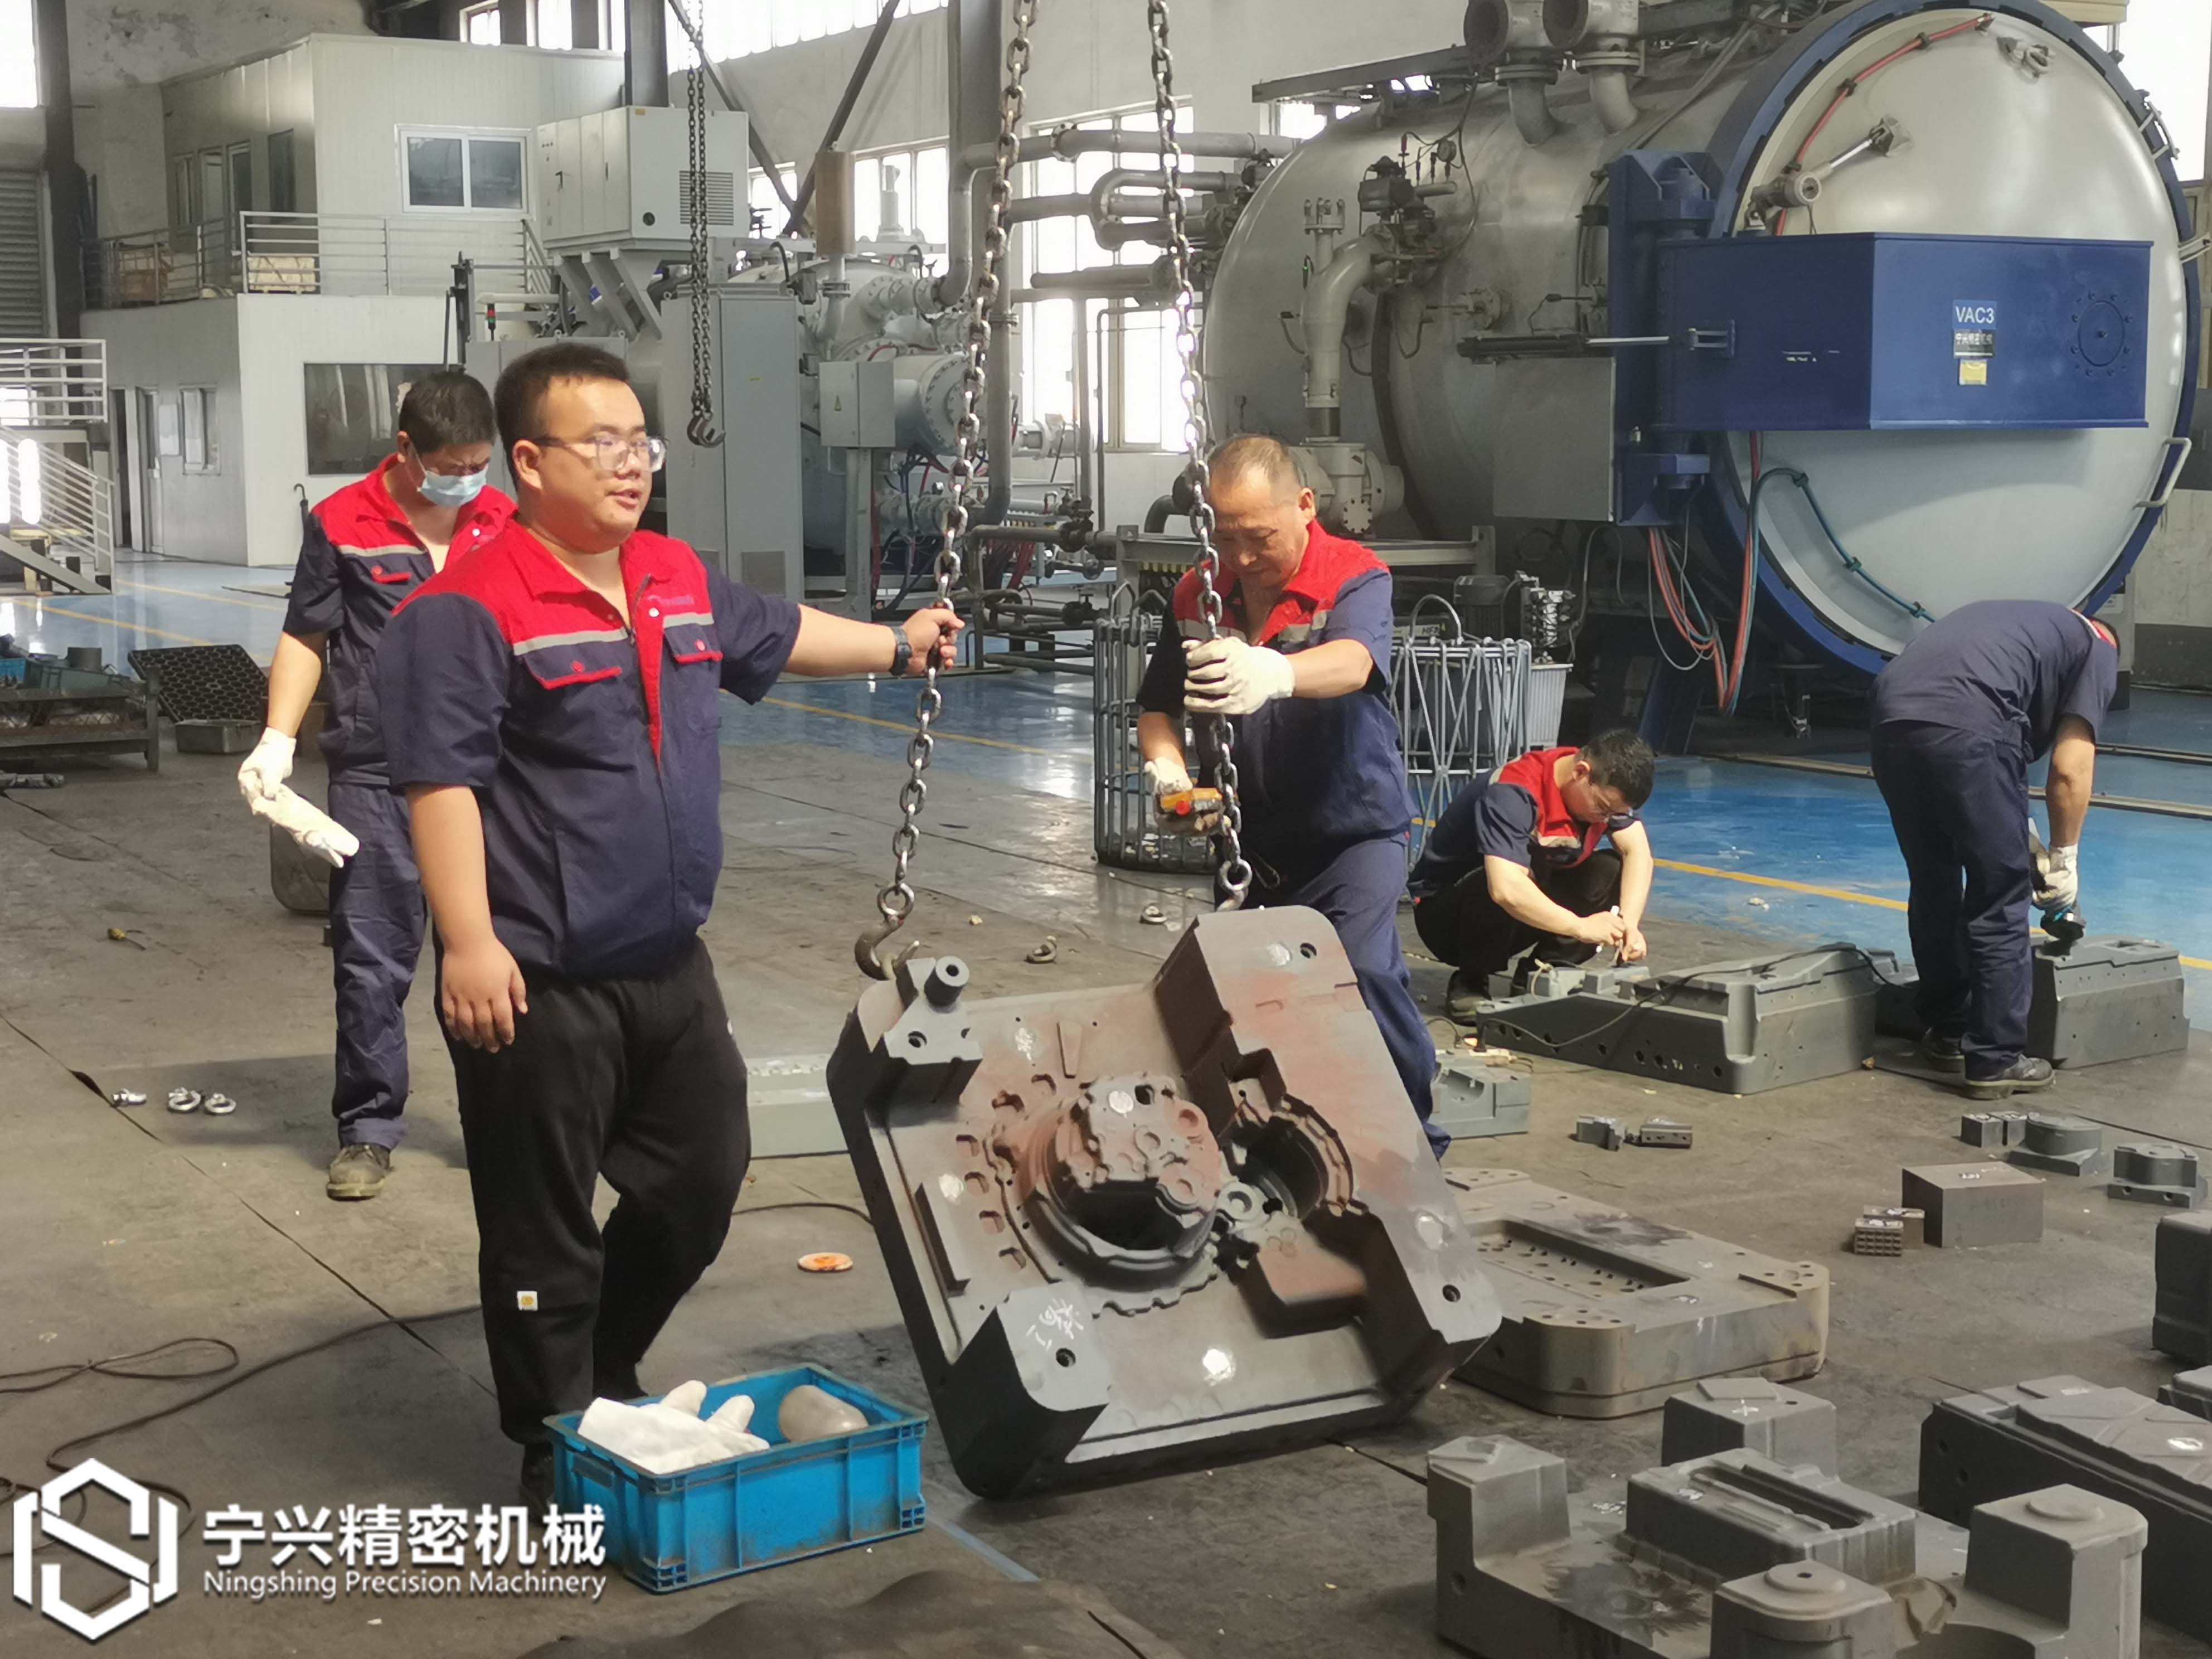 Ningshing remains passionate and dedicated in the heat of summer
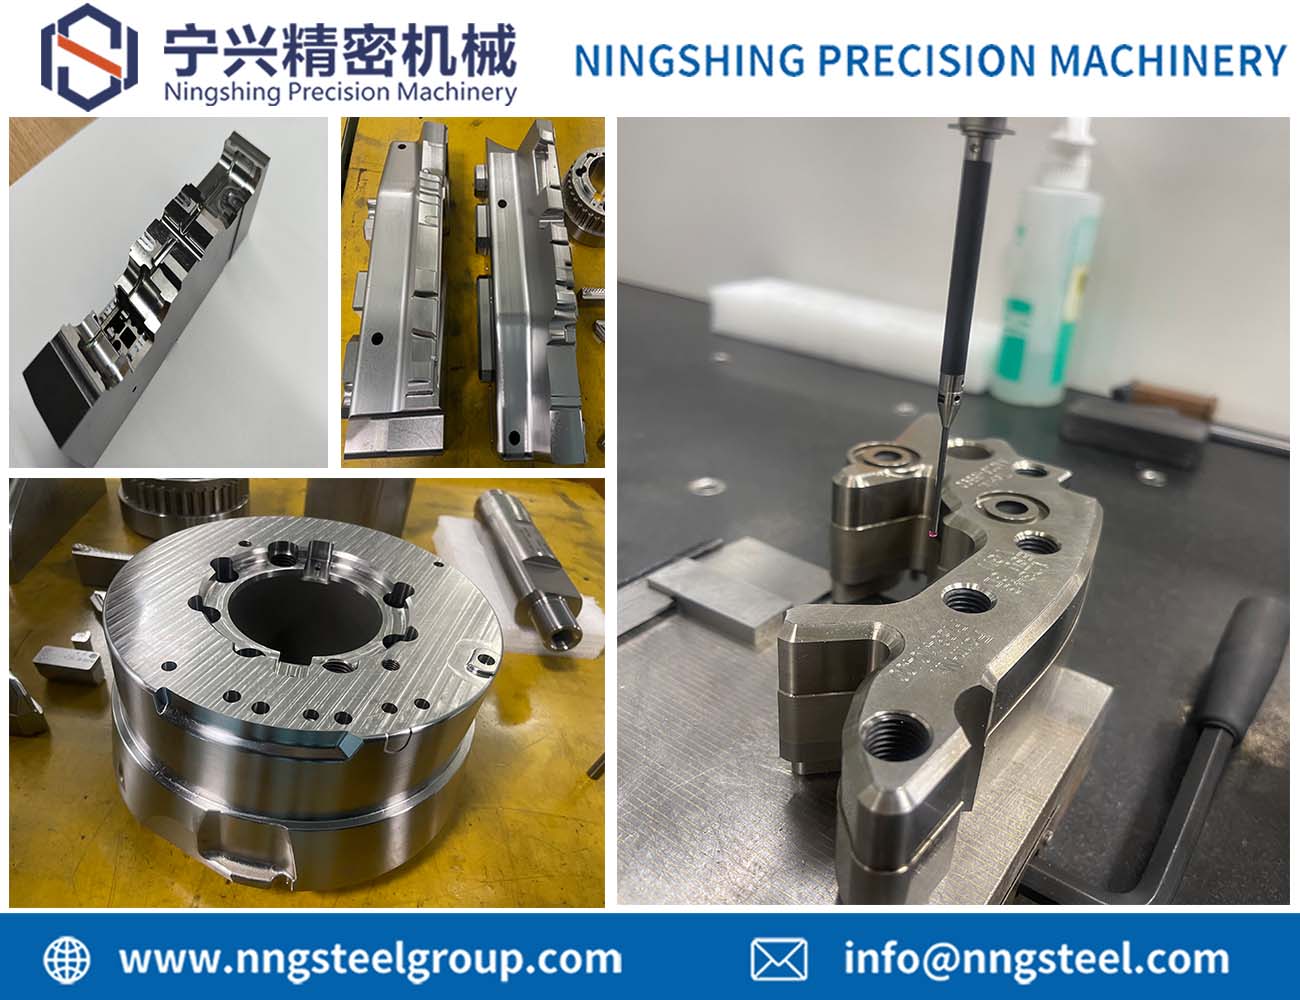 High Precision Mold Parts - Ningshing has the solution for you!
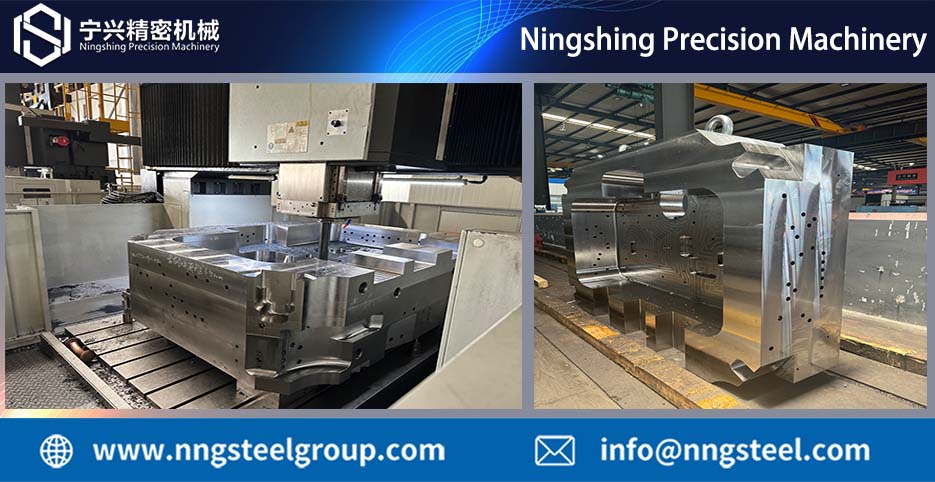 Mold processing case sharing
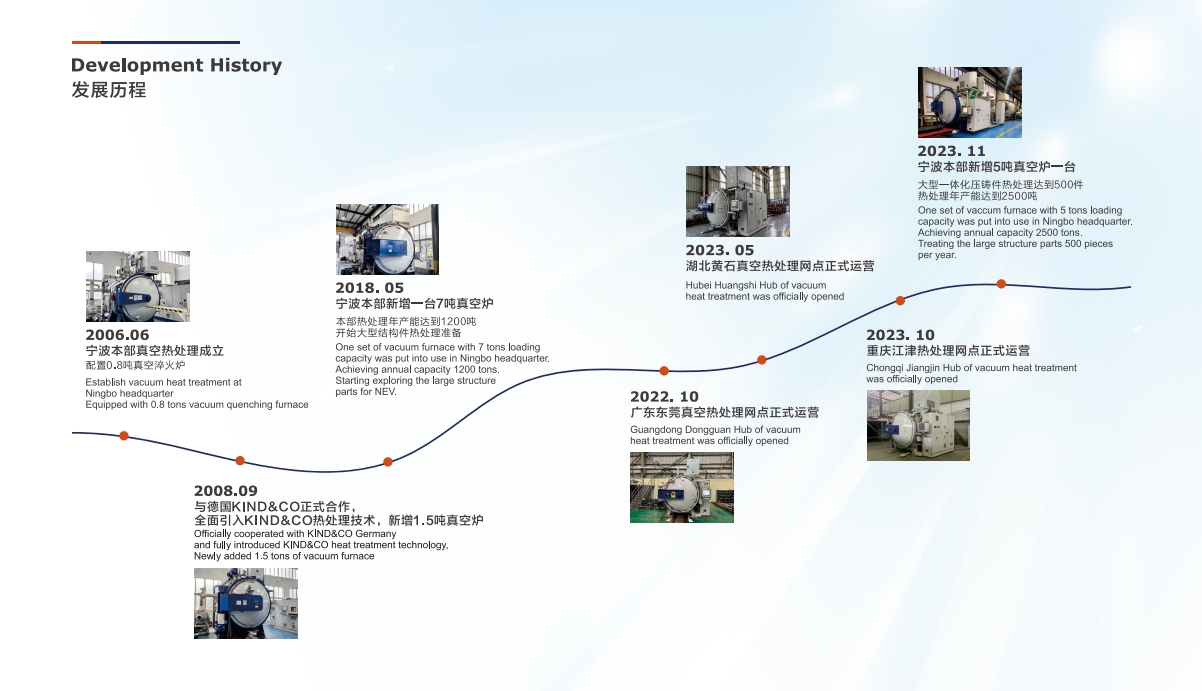 Exciting Milestones in Ningshing Heat Treatment Industry's Journey
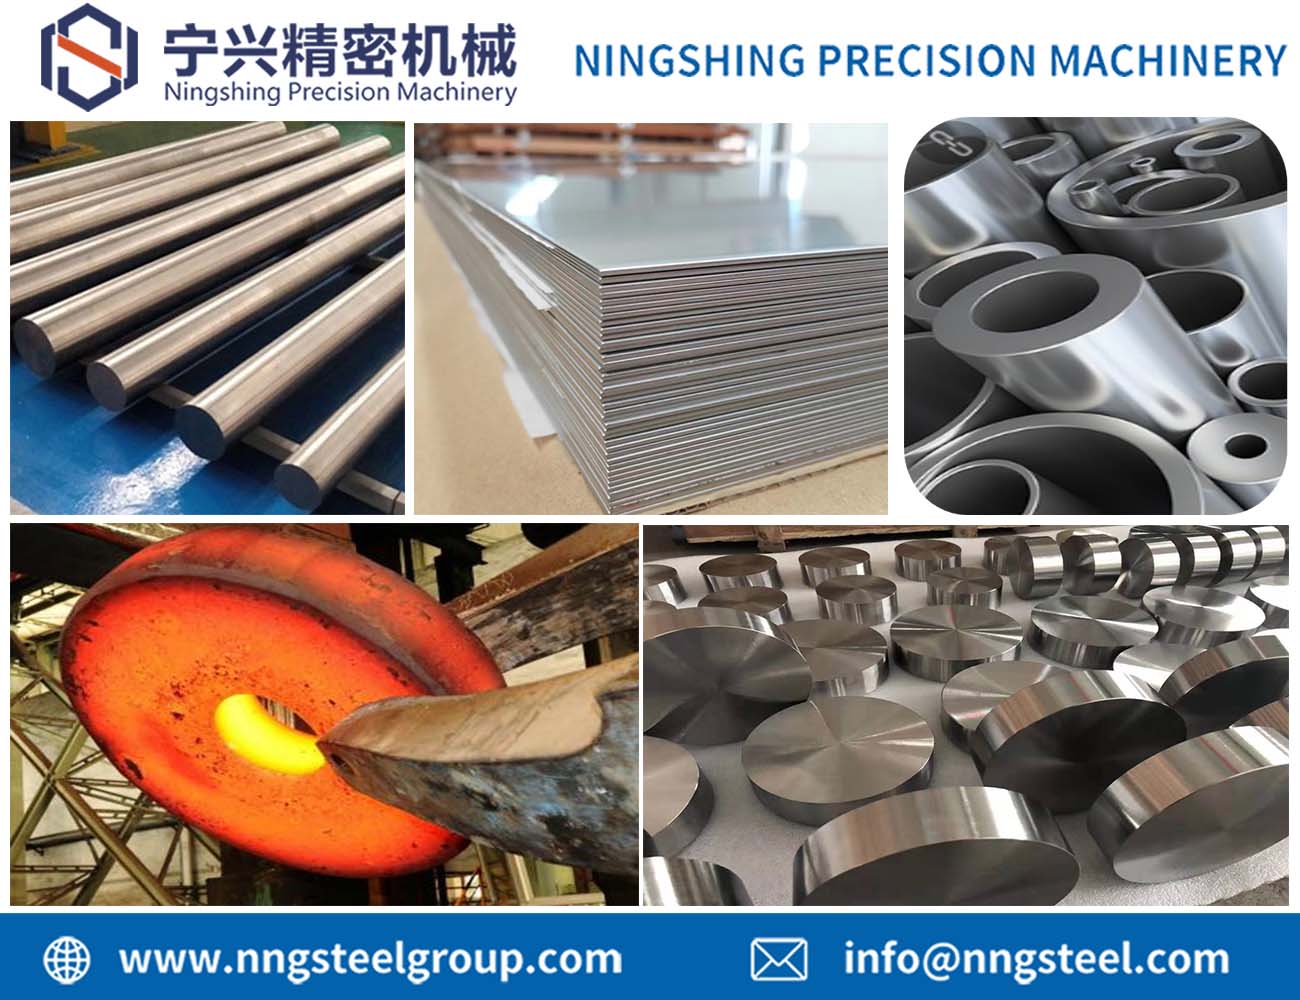 Ningshing New Product - SuperAlloys
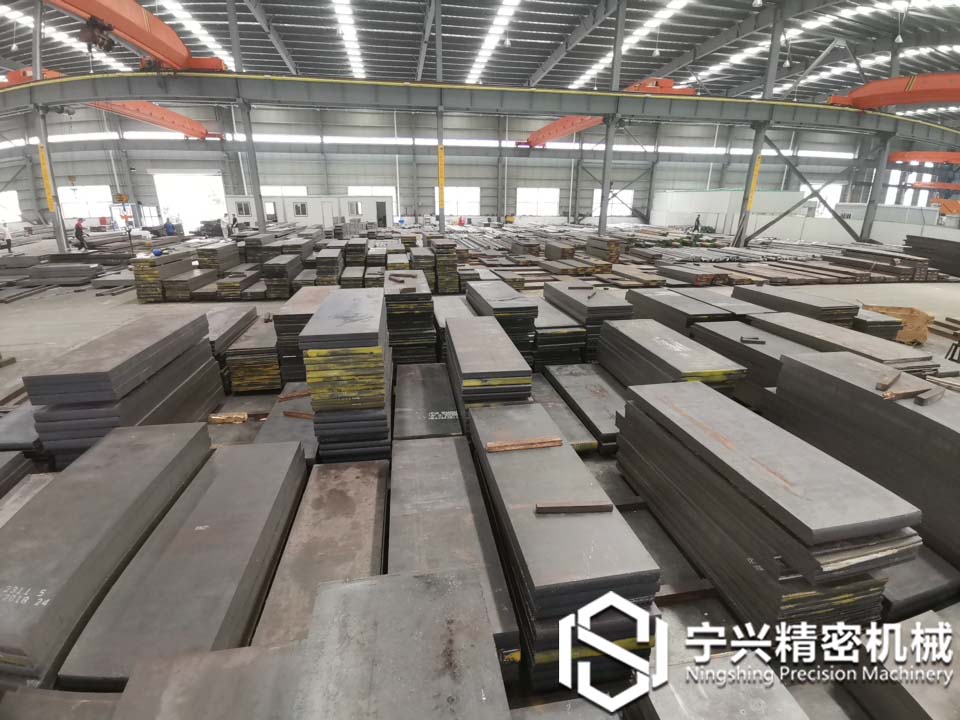 NINGSHING's tool steel stock base
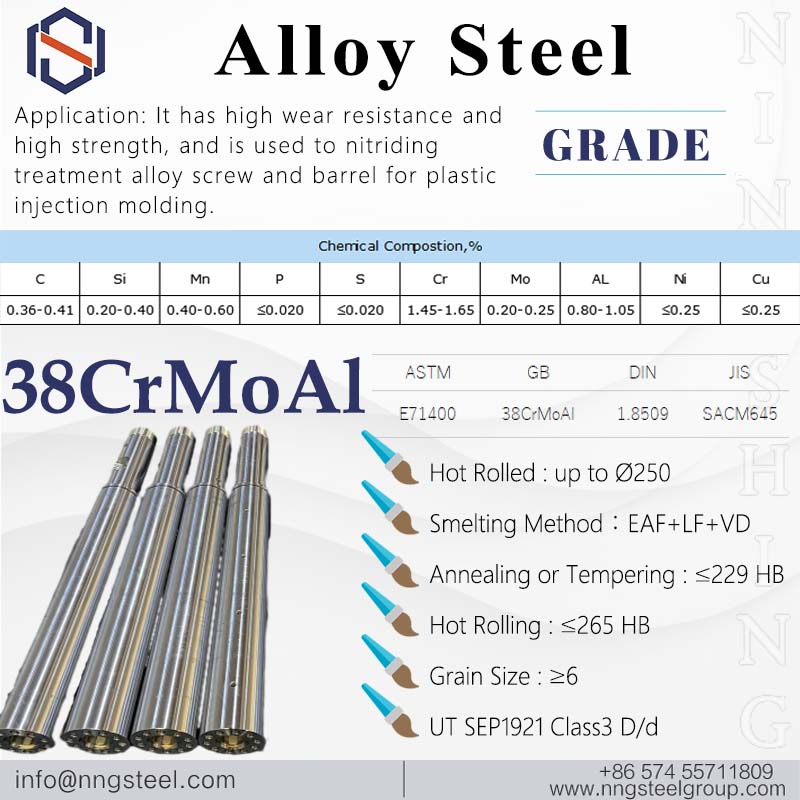 Alloy steel 38CrMoAl
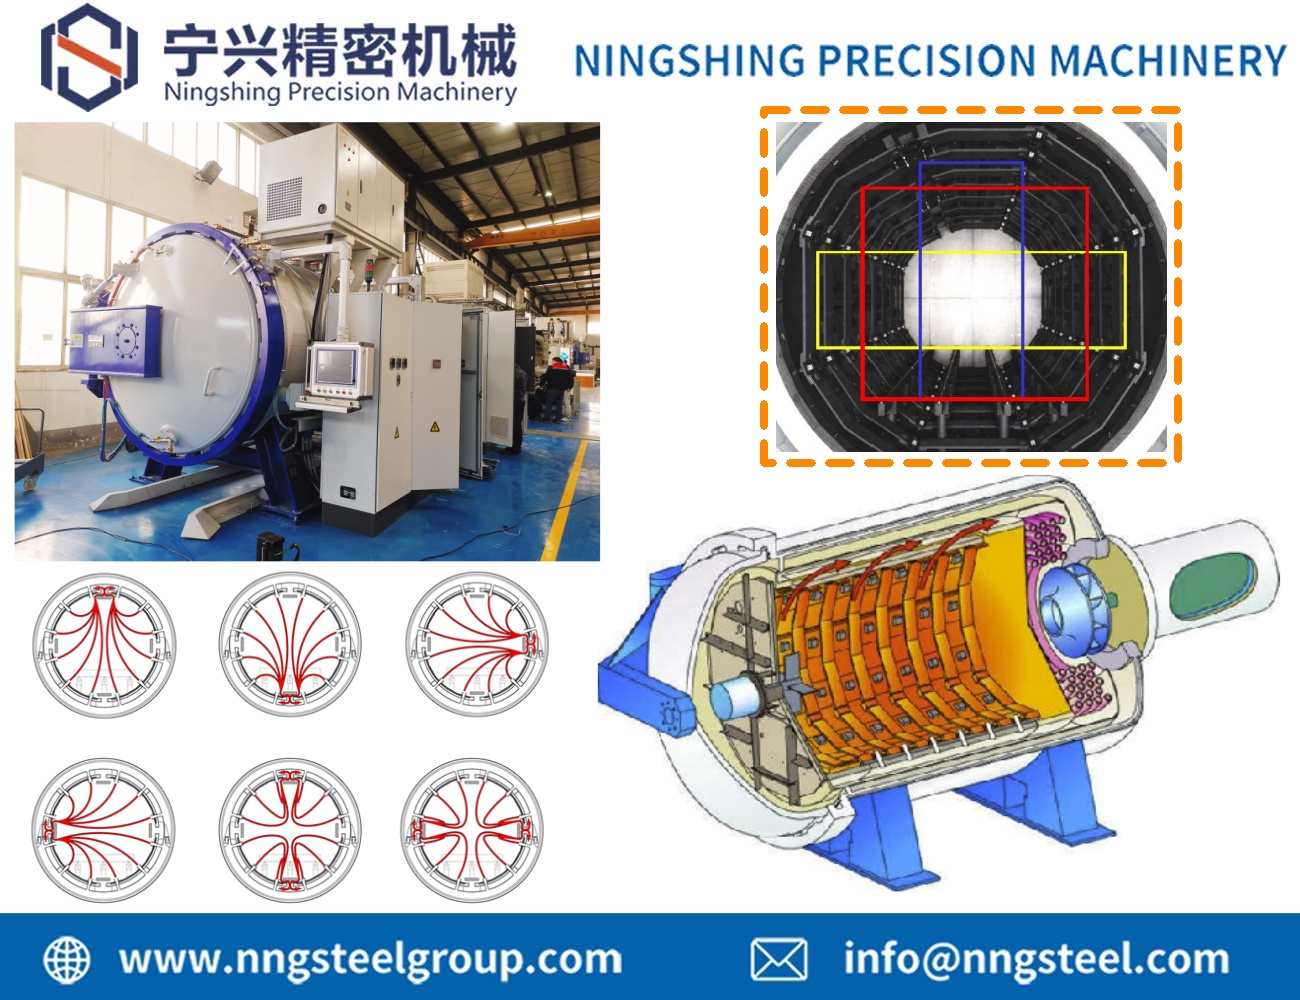 Ningshing's FUL121220 Vacuum Quenching Furnace: Setting New Standards in Heat Treatment Technology
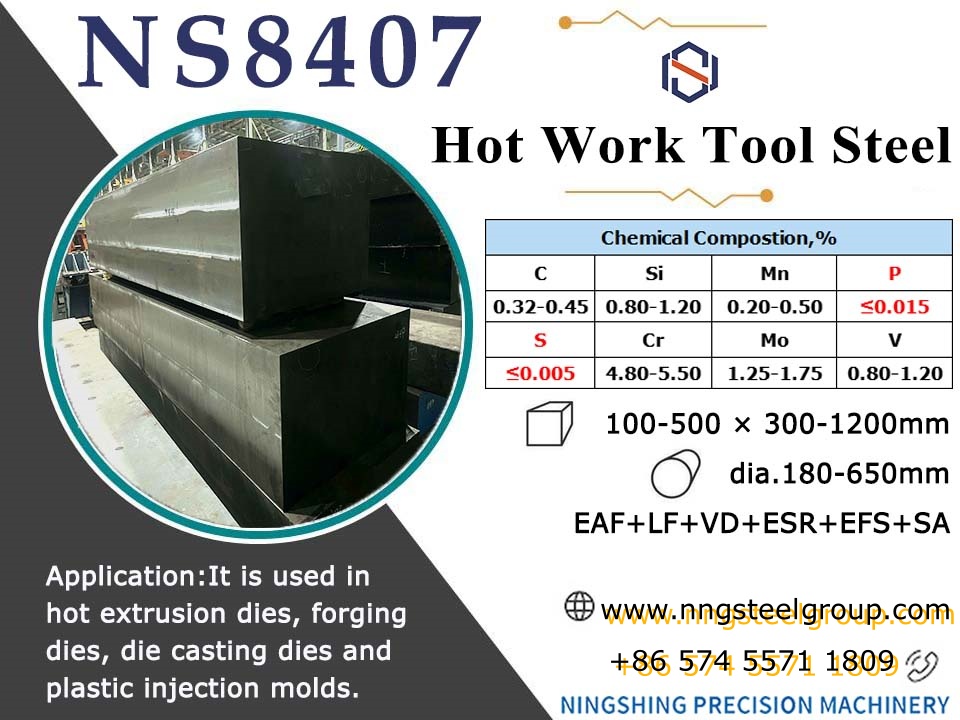 TOOL STEEL NS8407